Successful Projects

Precision Two-Shot Molding · Insert Molding

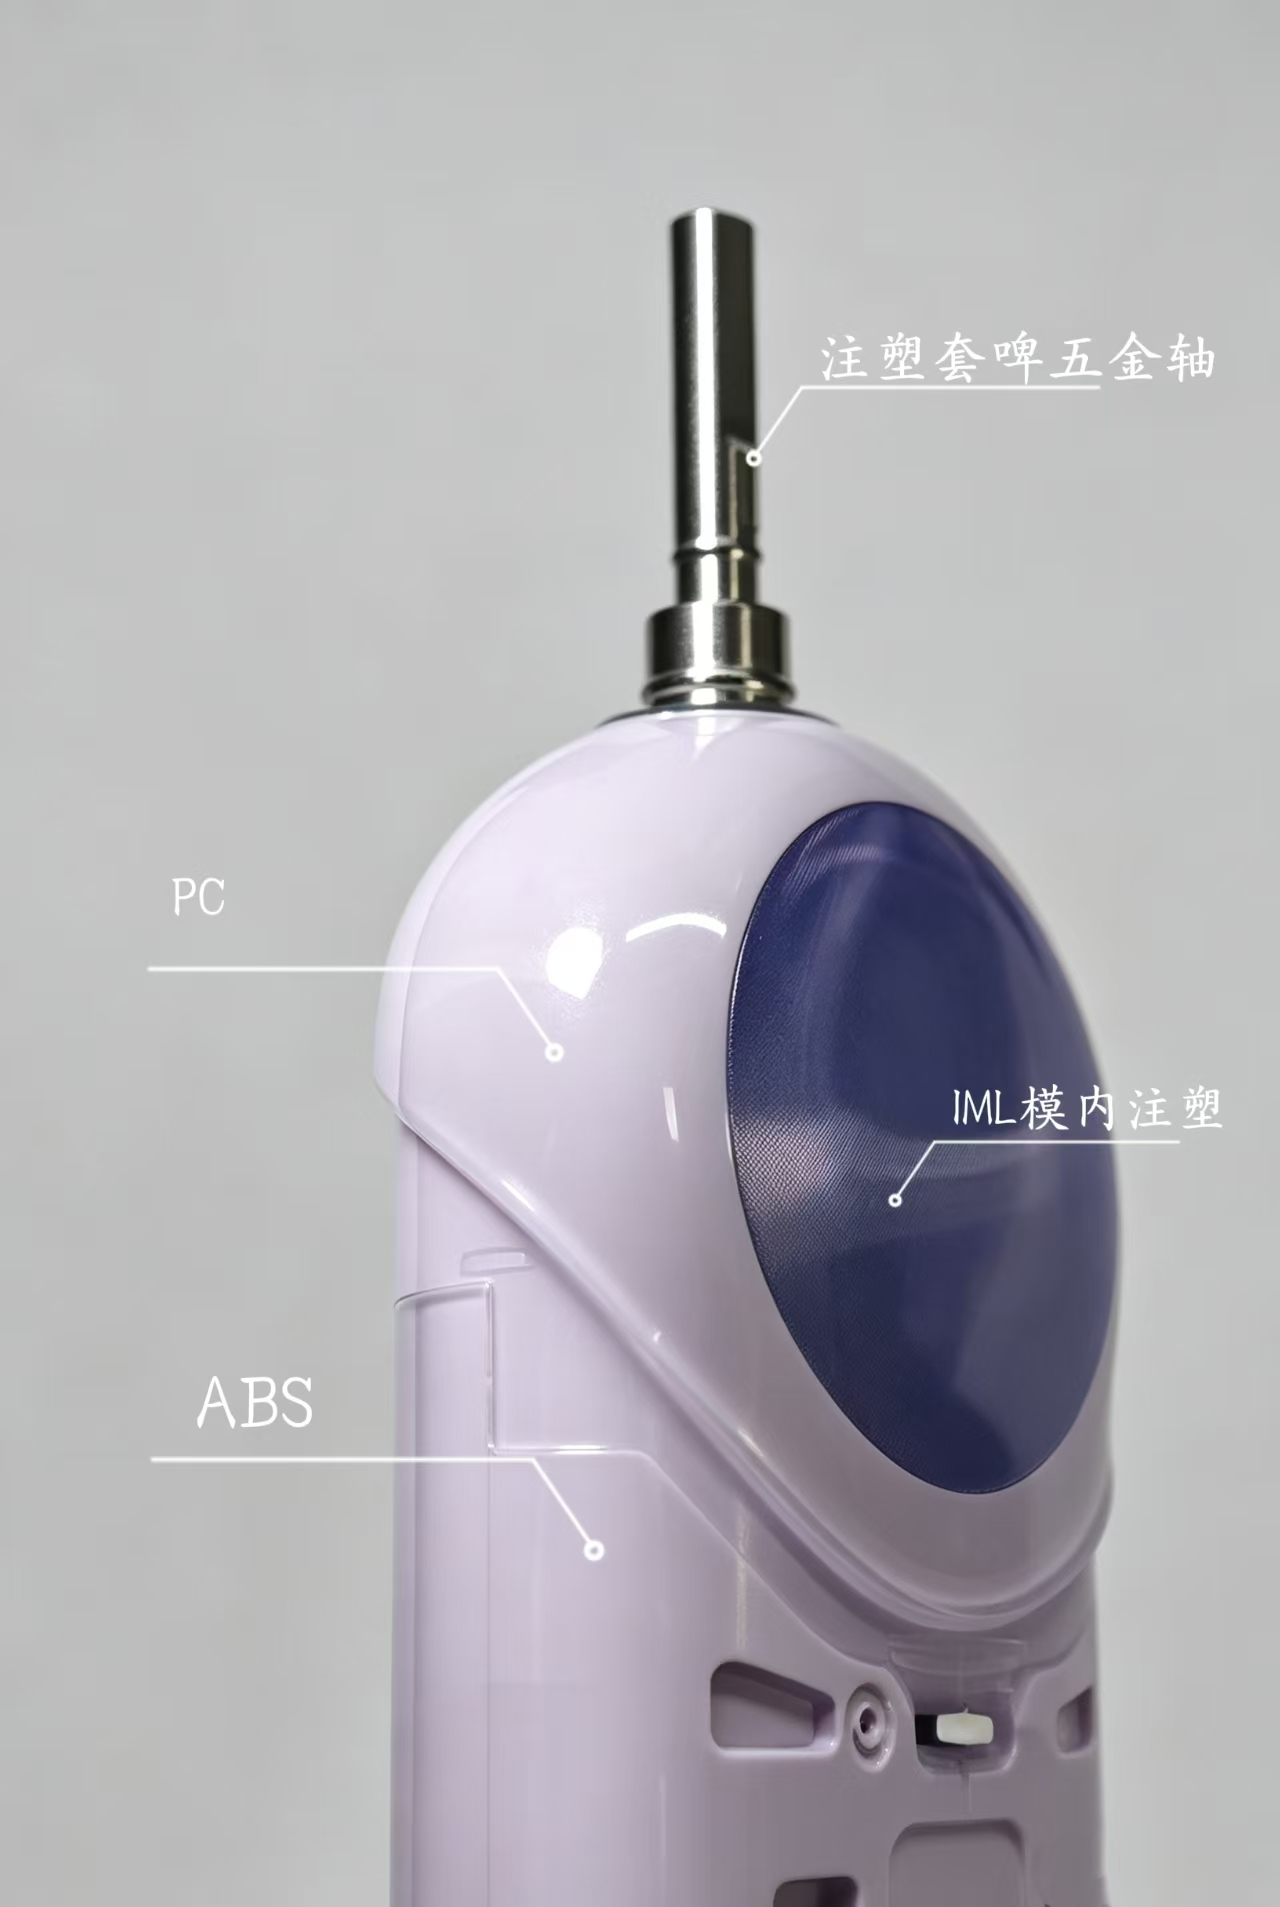
01Two-shot molded electric toothbrush pivot cover

Two-Shot Mold for an Electric Toothbrush Pivot Cover

Background

ABS558 in the first shot, overmolded with PC in the second. A hot-to-cold runner system and pin-point gates are combined with manually loaded metal shafts and IML decorative inserts, requiring stable molding for dental sterilization applications.

Challenges

PC and ABS differ in shrinkage and flow, leaving a narrow process window. Color mixing, weld lines and stress whitening must be controlled. Gate break-off must balance gate marks and pressure; thin inserts and IML require precise positioning and protection against deformation, crushing and movement.

Approach

Dedicated cavity venting and positive insert location; runner balancing through mold-flow analysis; separate mold-temperature control for ABS558 and PC.

Highlights

Insert molding, IML and two-shot overmolding in one process, with coordinated control of positioning, venting and the processing windows of both materials.
02POK and TPU two-shot molded drain hair catcher

Two-Shot Mold for a Drain Hair Catcher

Background

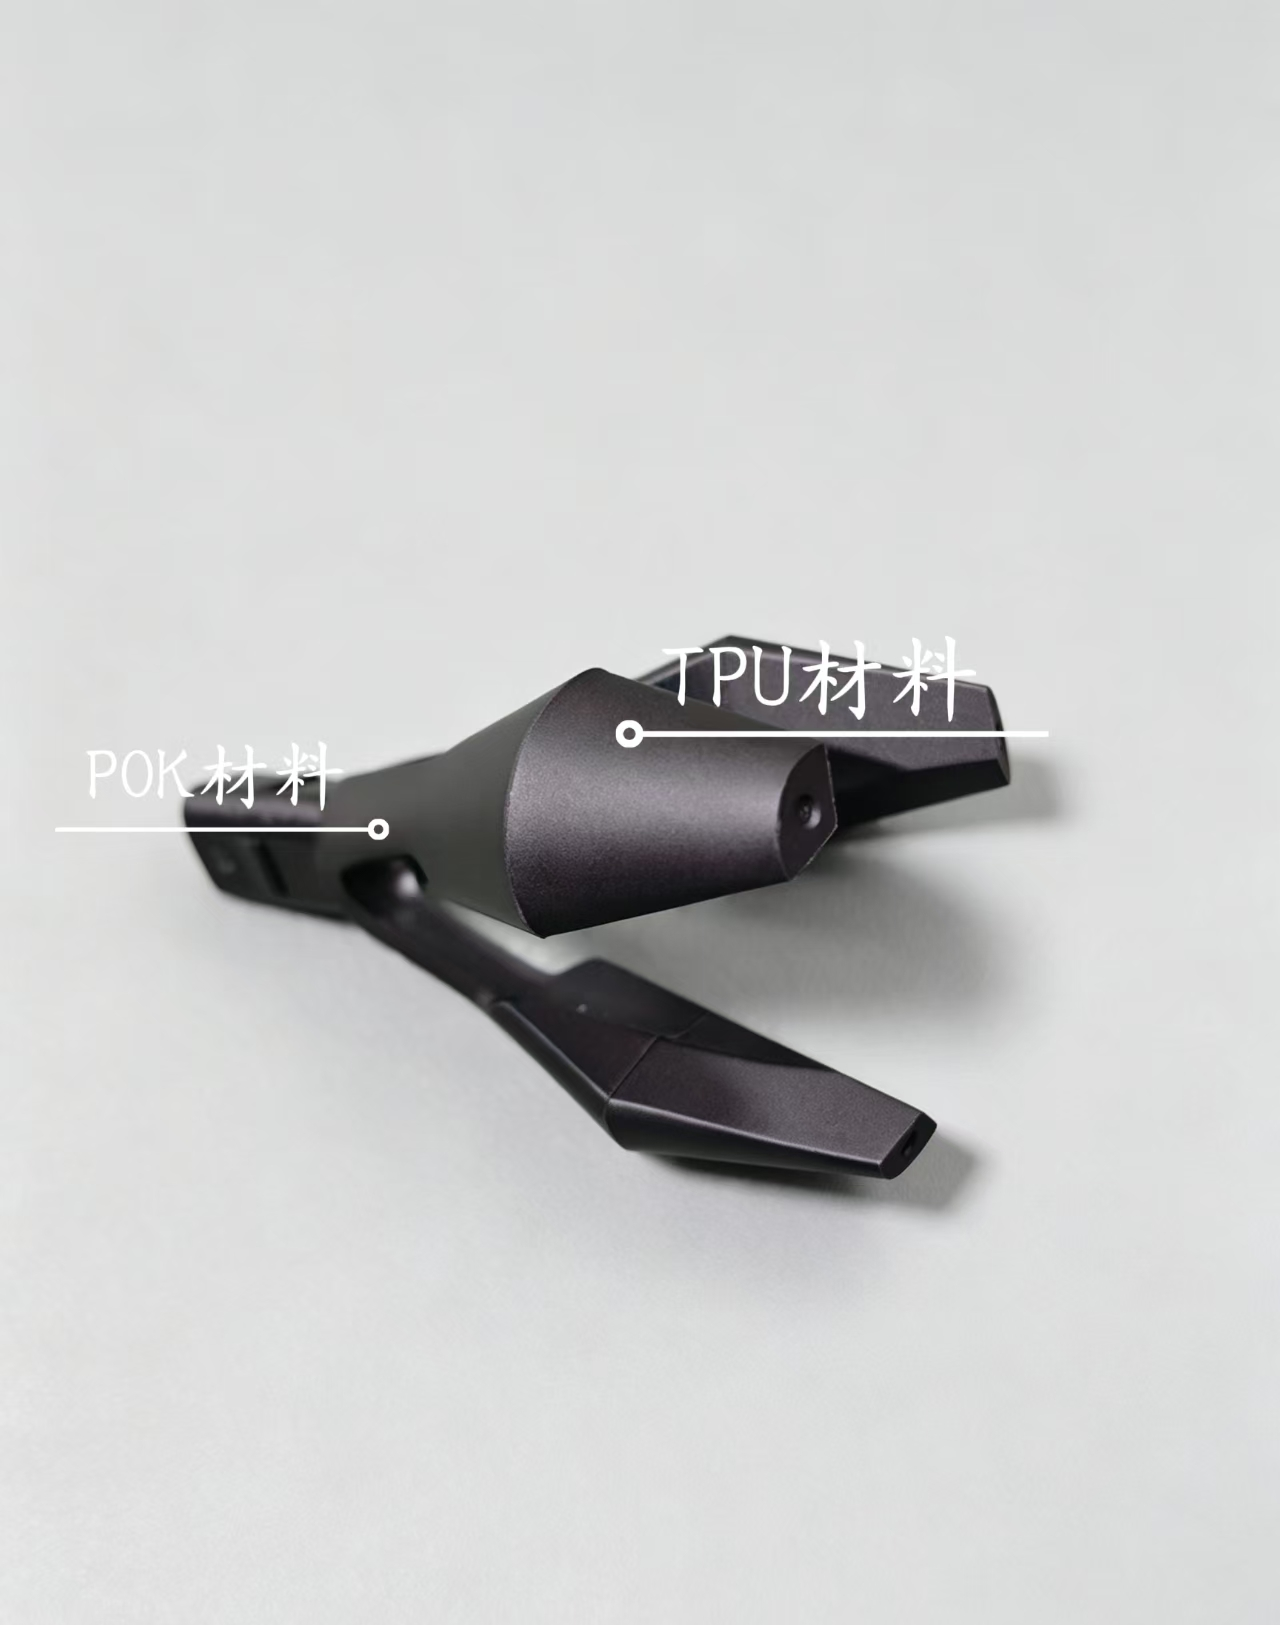
A rigid POK frame with soft TPU hair-catching claws, requiring resistance to hot water, cleaning products and wear, with secure overmolding.

Challenges

  • Balance TPU hardness with hair-catching performance, wear and chemical resistance.
  • Mold-flow analysis passed, but actual molding showed incomplete overmolding and short shots.
  • Feeding from inside the claws created a long flow path and trapped air, causing blisters and incomplete coverage.

Solution

  • Use polyether-based TPU, Shore A 75–85.
  • Move the soft-material gate to the top to shorten the flow path and synchronize coverage.
  • Add undercuts and dovetail grooves to the POK frame for stronger mechanical interlocking.
  • Optimize venting, mold temperature and runners.